
Chemical Composite Hose Sets New Standards for Safe Fluid Transfer in Chemical Industries
Release time:
2025-04-02
Author:
Source:
Abstract
The latest chemical composite hose is revolutionizing fluid transfer systems in the chemical industry. Engineered to meet the rigorous demands of transporting aggressive chemicals, oils, and solvents, this new hose provides superior strength, flexibility, and resistance to corrosion and chemical damage.
Manufactured with multiple layers of advanced composite materials, the chemical composite hose is specifically designed to prevent leaks and withstand the toughest chemical environments. Its unique construction not only ensures long-lasting durability but also maintains flexibility for easy routing, making it an ideal choice for refineries, chemical plants, and hazardous material transport.
Key Features:
- Superior Chemical Resistance: Built to handle a wide range of chemicals, including acids, alkalis, and solvents, without degradation or contamination.
- Multi-Layered Construction: Reinforced with durable layers that provide strength and prevent leaks, while maintaining excellent flexibility.
- High-Performance Safety: Designed to reduce the risk of chemical spills, offering improved safety for operators and the environment.
With enhanced safety, durability, and performance, the chemical composite hose is the top choice for industries that require reliable and safe fluid transfer of aggressive substances.
Recommended Reading

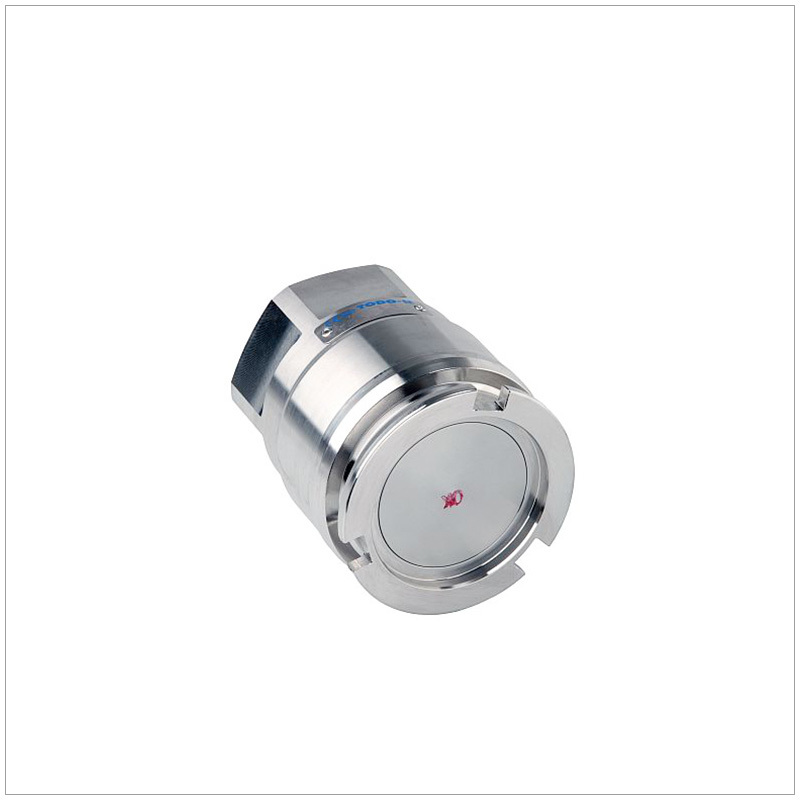
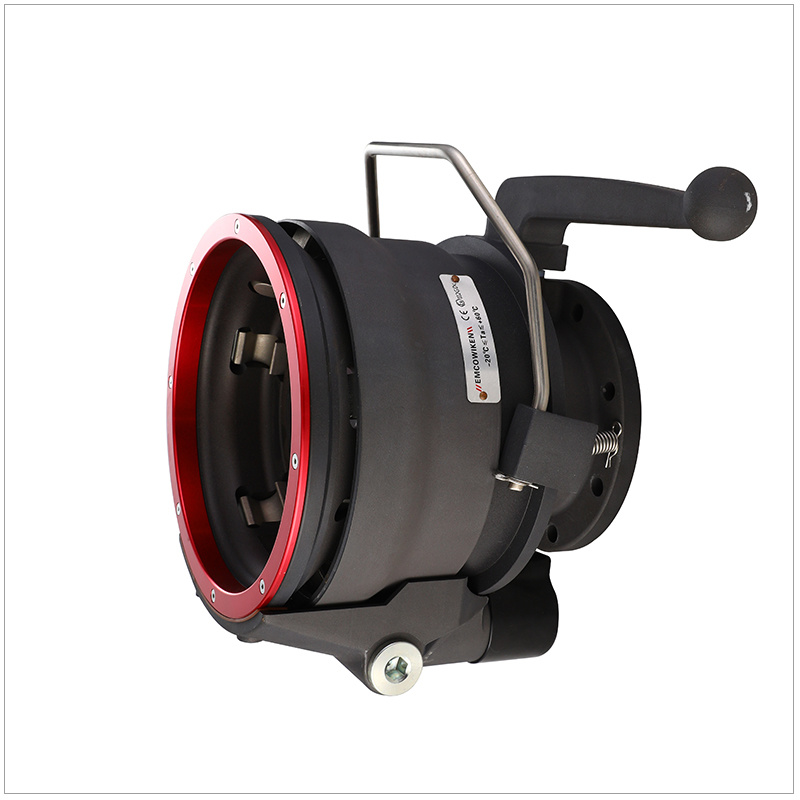

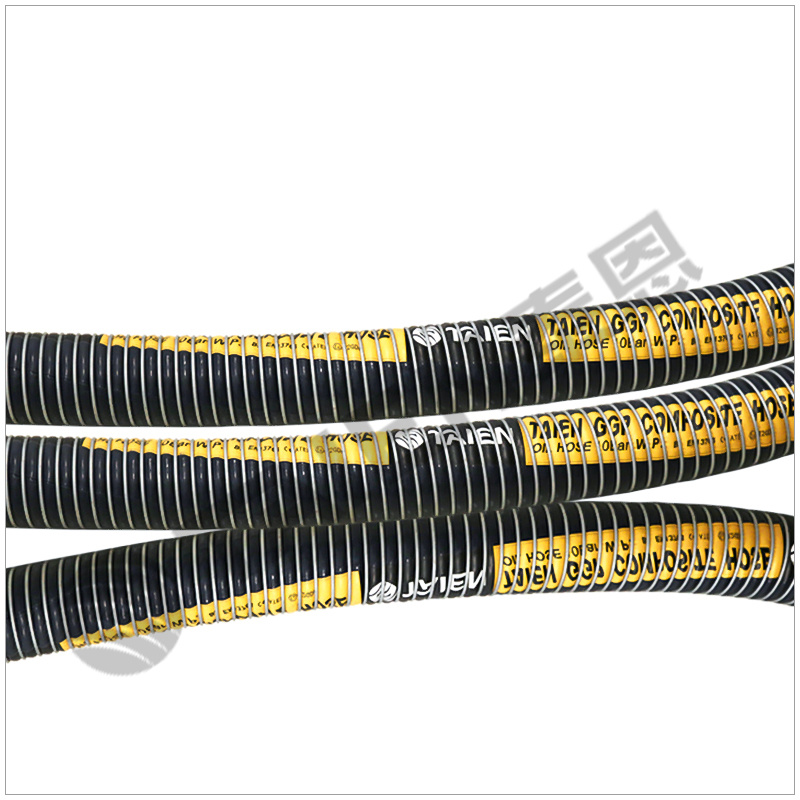
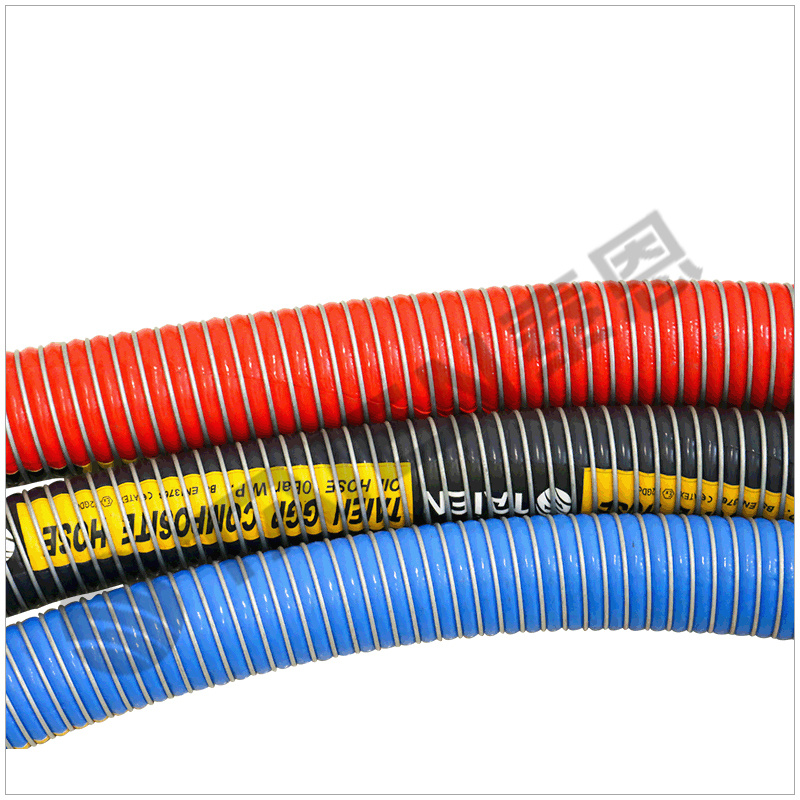
Guangdong Taien Fluid Control Equipment Co., Ltd. is a professional manufacturer and supplier of fluid transmission equipment, focusing on various types of gas stations, chemical plants, oil refineries for more than 20 years It is a state-level high-tech enterprise that provides high-quality complete sets of equipment and surrounding safety and environmental protection facilities.


Product Series
Contact us
+86-020-34008936
Unit 3314, No 1020 Xingangdong Road, Haizhu, Guangzhou China.
Mobile Website
